Xinba Town, Yangzhong, Jiangsu, China
HONGRIND Precision Abrasives Request a Quote
Bearings

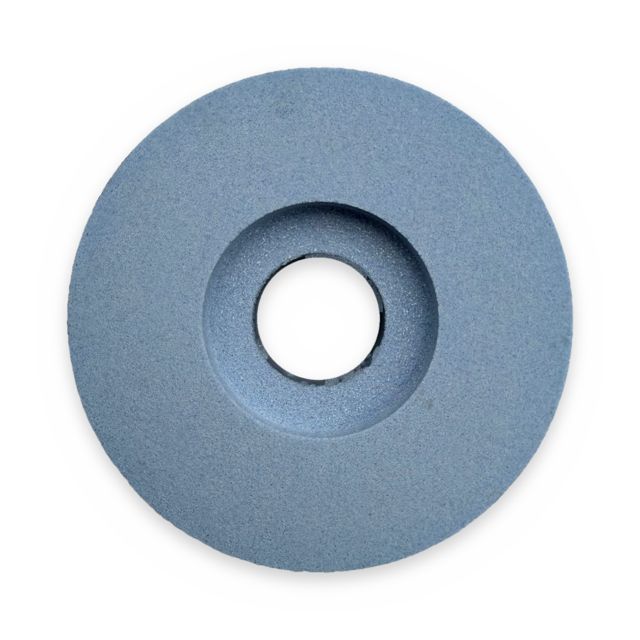
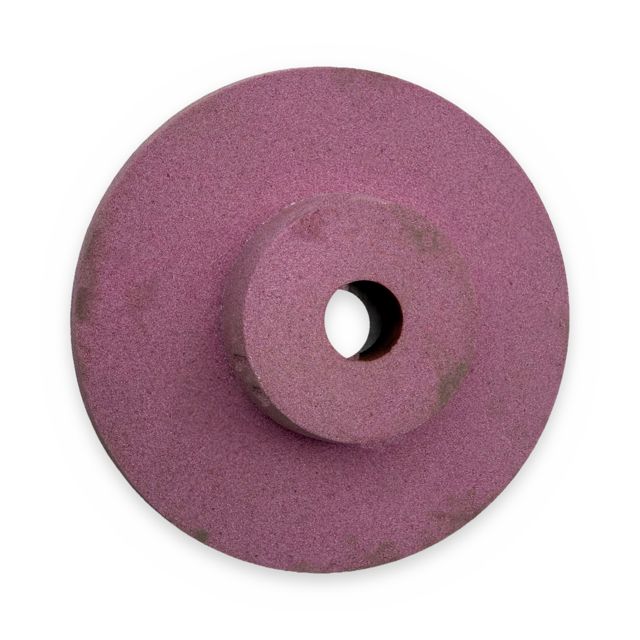
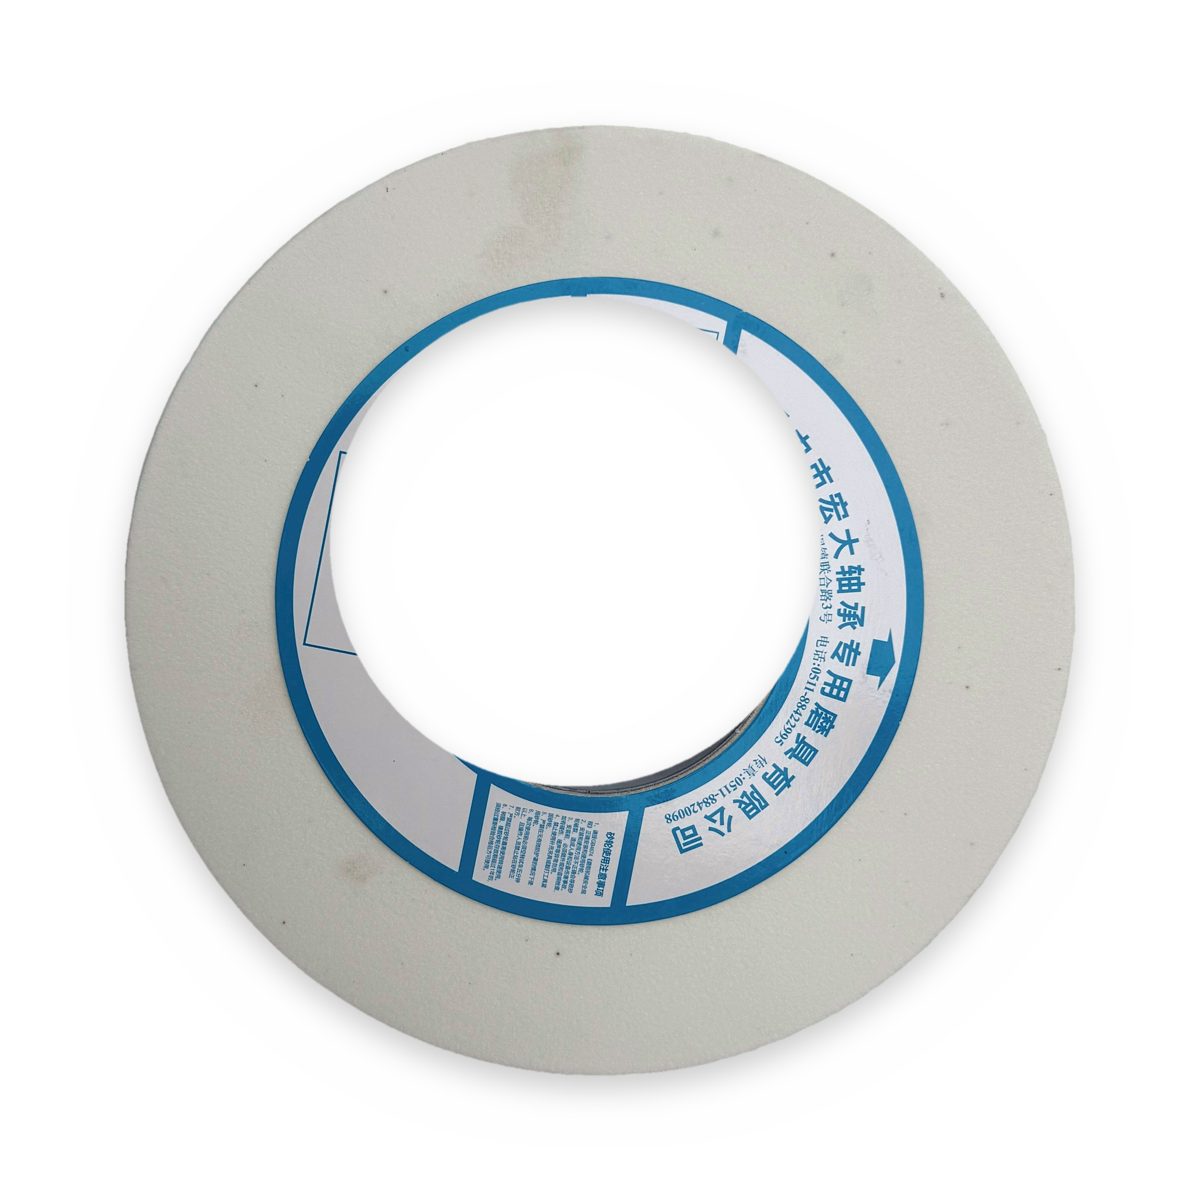
Outer Ring Raceway Grinding Wheels

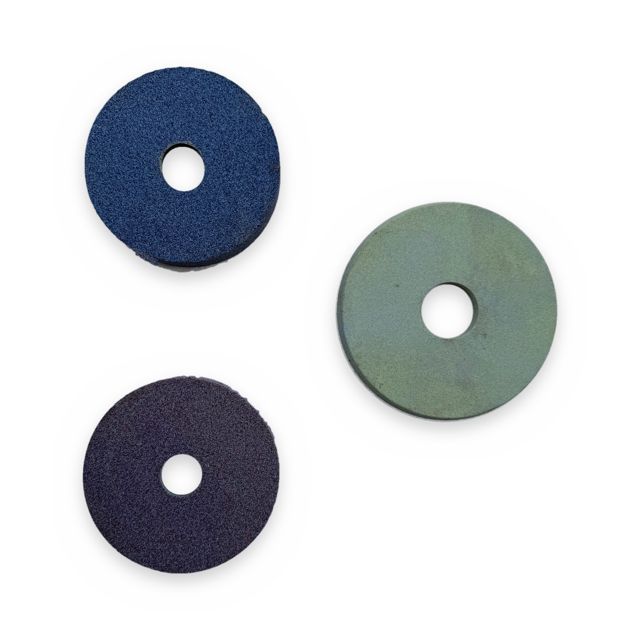
Vitrified wheels for grinding the raceway inside bearing outer rings, including flange raceways of automotive hub bearings.

Our HG series combines imported SG ceramic abrasive with our own low-temperature, high-strength S1 bond, allowing grinding at up to 80 m/s with longer dressing intervals. Our HC composite CBN wheels can be dressed with your existing diamond pen instead of a CBN diamond roller.

Options

Abrasive
White fused alumina, SG ceramic alumina (HG series), composite CBN (HC series)
Bond
Vitrified, incl. low-temperature high-strength bond S1
Working speed
Up to 80 m/s depending on specification
Profile
Made to your drawing or sample wheel

Typical applications

  • Deep groove ball bearing outer rings
  • Hub bearing outer flange raceways
  • Angular contact bearing outer rings

For a fast quote, send us

  • The marking on your current wheel (a photo of the label is fine)
  • Wheel dimensions or a drawing
  • Workpiece and material, machine model
  • Your current wheel life and what you want to improve
Proven in production

Related grinding cases

C&U Wuhu Automotive Bearing

Hub bearing line — outer flange raceway

HG/F80#KV 1-70×14×20 80m/s · HG/F80#KV 1-70×24×20 80m/s
31.5 → 26 scycle time
2×wheel life

Imported SG abrasive with our low-temperature, high-strength S1 bond allows 80 m/s grinding. Dressing interval extended from 6 to 10.
Jiangsu Tianchi Bearing

Bearing ring internal raceway grinding

HC/F120#MV 1-17×15×6 80m/s
5 → 50dressing interval
NoCBN diamond roller needed

Our composite CBN wheel is dressed with the existing diamond pen, so no costly CBN diamond roller is required. Diamond pen wear and wheel changes drop sharply.

Chongqing Changjiang Bearing

Hub bearing line — raceway grinding

98A/F100/60#L-KV 1-70×(20+7)×20 60m/s · SAWA/F100/60#L-MV 1-64×(16+7)×20 60m/s
Compositetwo-zone wheel
0burn or chatter marks

Different abrasives and hardness grades are formed into one wheel, each matched to a zone of the raceway. Wheel wear drops, life increases, and the load on superfinishing is reduced while profile accuracy improves.